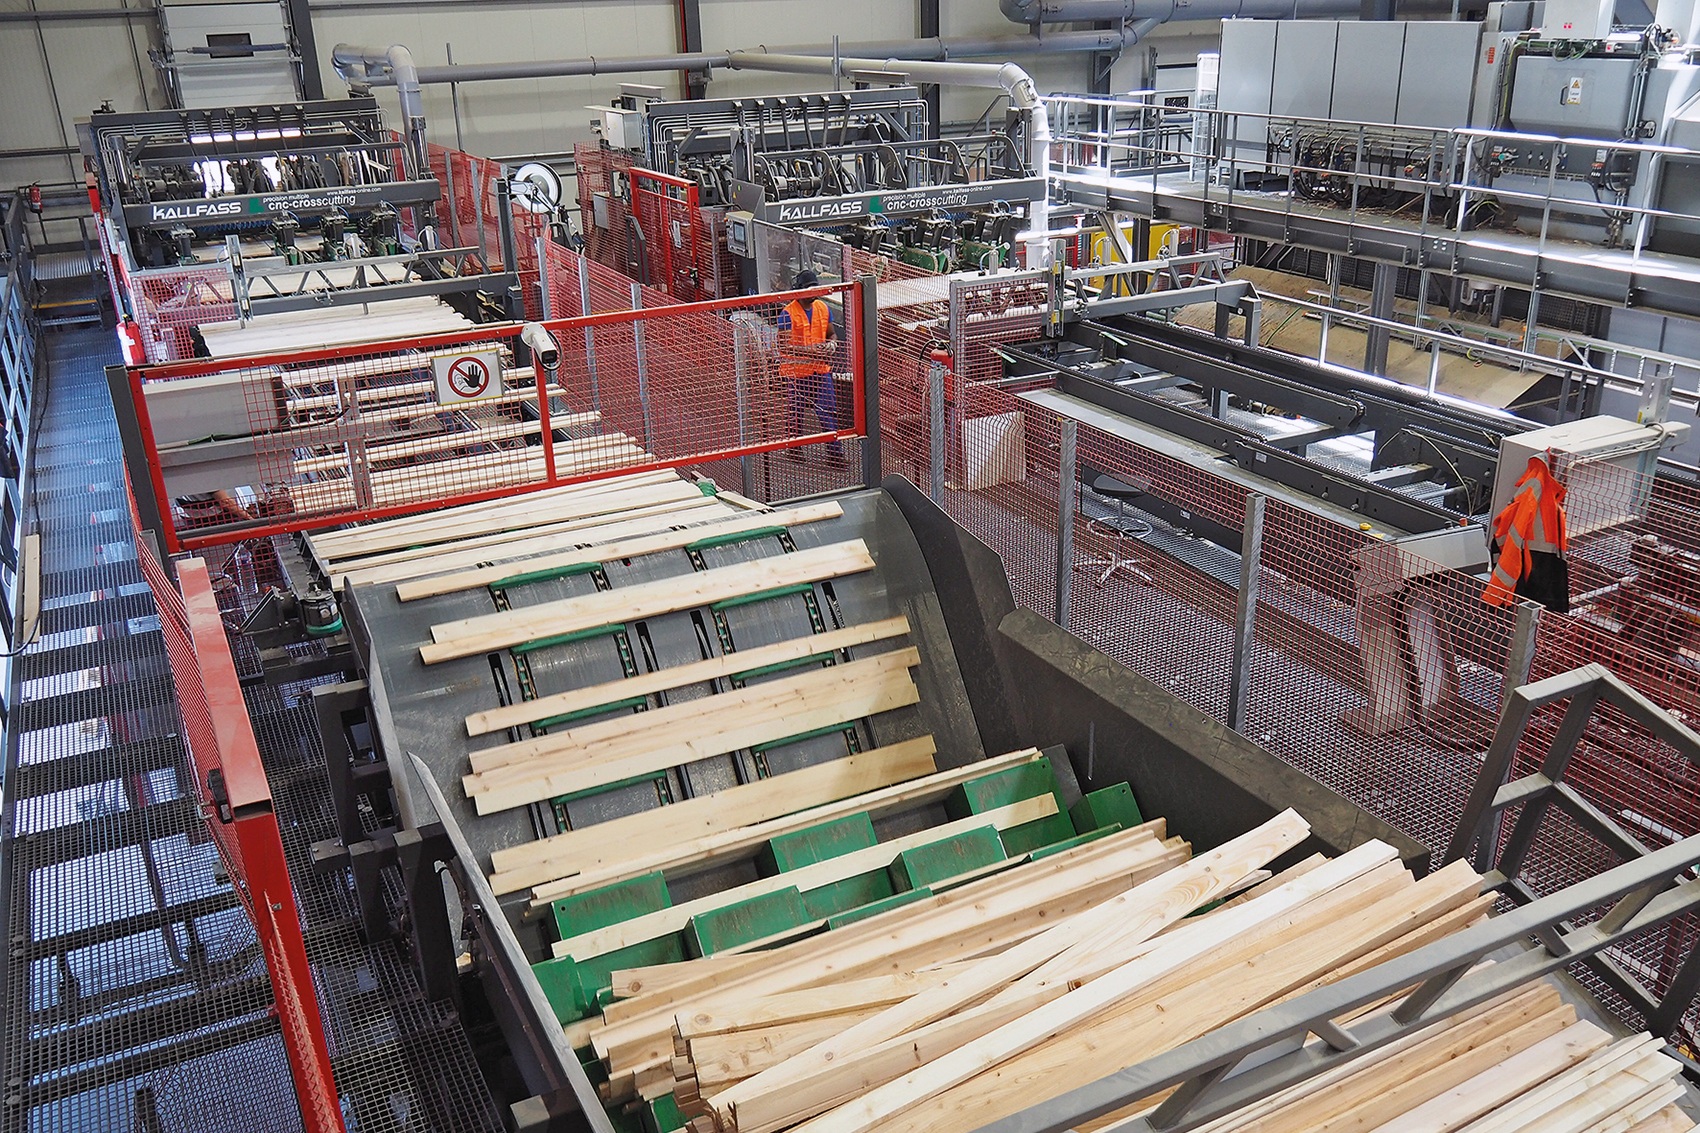
Kallfass Stapel- und Sortierwerk, stacking and sorting line

Stapelanlagen für Palettenbretter EN Stacking systems for pallet boards

To increase supply to the company's in-house pallet production, Groupe François has invested in a new sawmill at its headquarters in Virton/BE in recent years. Based on years of successful cooperation, the company once again selected Kallfass (based in Baiersbronn-Klosterreichenbach, Germany) for the sorting and stacking system.

Groupe Franςois produced around 3 million pallets per year in Virton, Belgium. With a small-diameter timber sawmill operating since 2006, the company previously produced around 75,000 m³ of sawn timber annually for its own further processing. "We had to buy in about 20%. In addition, we were only able to cut diameters up to 25 cm", explains Nicolas Quoirin, sawmill manager at Groupe François. For this reason, the decision was made a few years ago to expand the sawing capacity. The vast majority of the sawn timber goes into pallet production, with only a small portion of the goods sold on the open market.

The log yard, which was previously located in the centre of the mill, was moved to the edge of the site. Groupe Franςois was then able to build the sawmill on the area that had been freed up. What sounds relatively "simple" in a few words has been a years-long undertaking. After the new log yard featuring the Holtec gantry crane was commissioned first (see Holzkurier issue 51-52/2024, pp. 18–19), the startup of the new sawmill followed in autumn 2025. For the primary cutting technology (quadro band saw, BNK edging system, and NKU resaw), the choice fell on EWD, based in Altötting, Germany. The downstream sorting and stacking system was supplied by Kallfass. "The mechanisation and sorting in the small-diameter timber plant had already been supplied by Kallfass. Due to our good working relationship, we chose Kallfass once again", explains Florent Vanlaetem, project manager at Groupe François. "We know the company and its efficiency, and right from the start we were confident that Kallfass would execute everything according to our expectations."

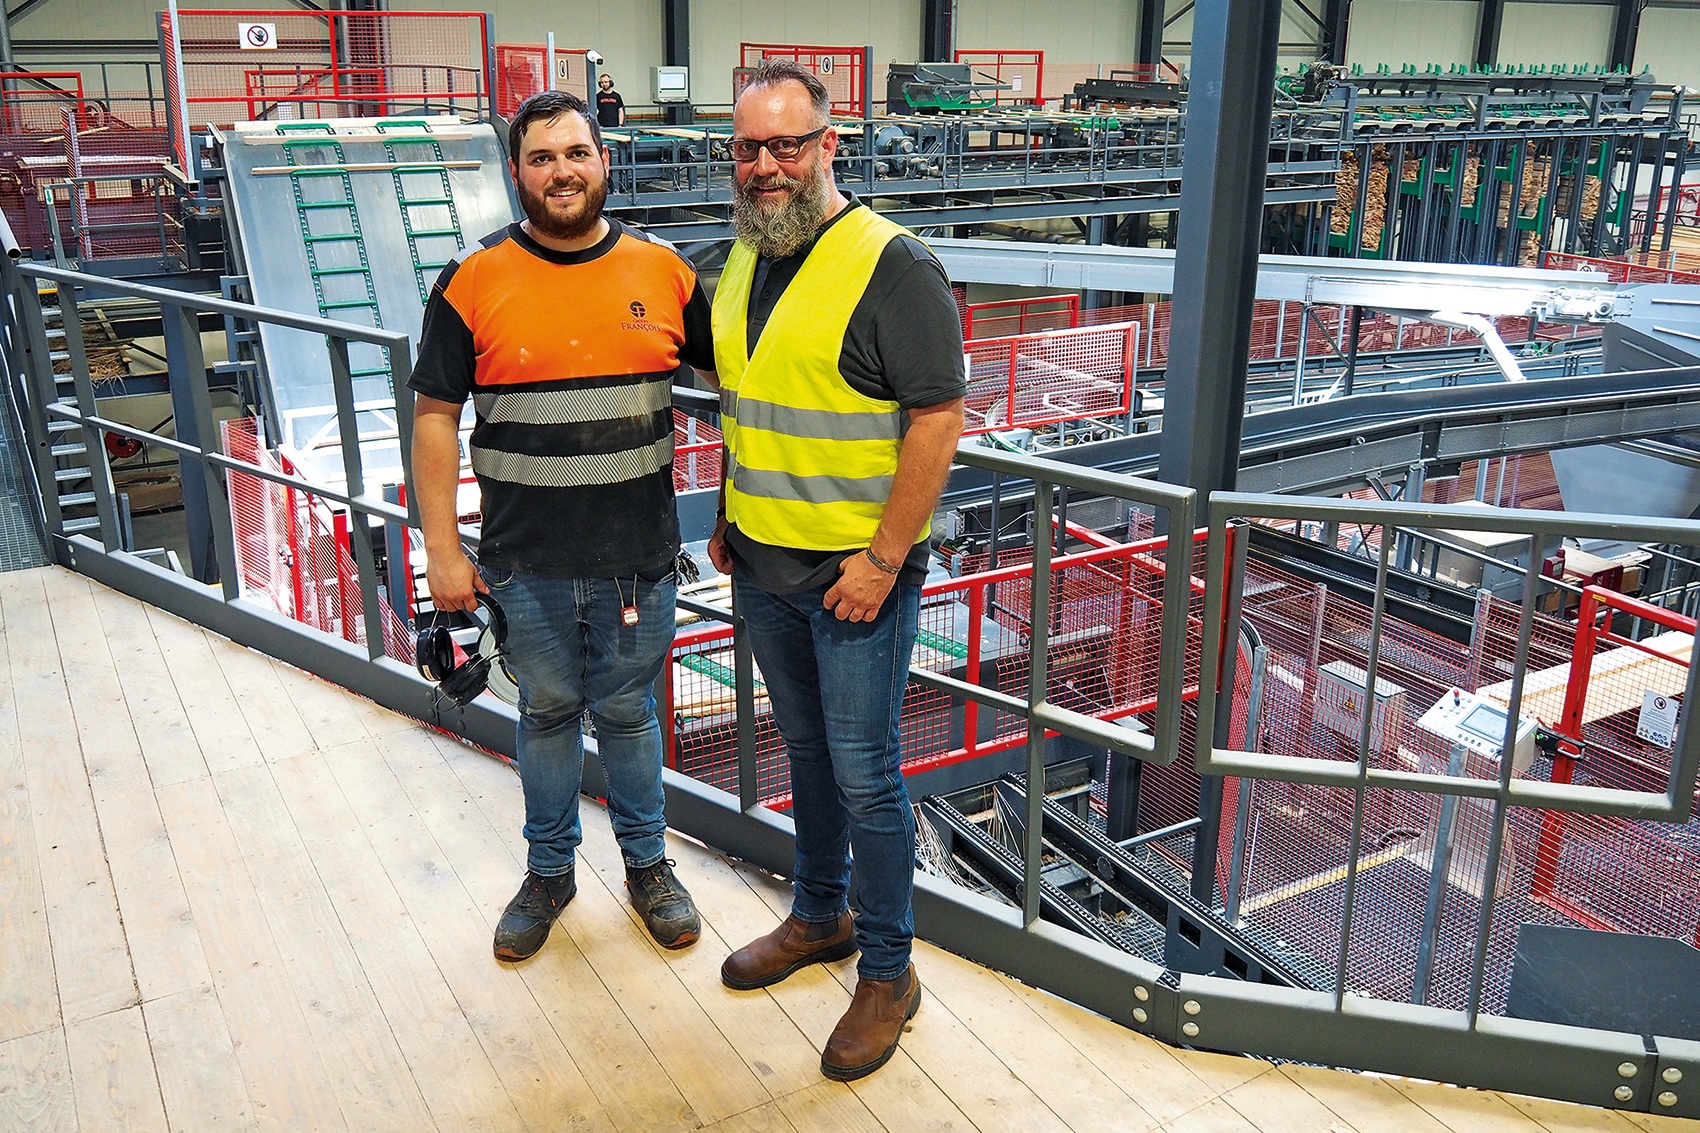
Showing the new sorting and stacking system from Kallfass: Groupe Franςois sawmill manager Nicolas Quoirin and Matthias Link from Kallfass (from left)

Flexible sorting

"Originally, only one line with box sorting and stacking was planned for the project. "However, since cutting pallet boards often produces identical dimensions, Groupe François decided to install a separate stacking system for the timber from the NKU resaw", explains Matthias Link, project manager at Kallfass. "This system is now the main line. However, if there are any faults or maintenance is necessary, we can move the goods to the second sorting line. "This makes us very flexible and allows us to minimise downtime", Quoirin emphasises as the main advantage. The corresponding information regarding which timber goes to which line comes from the EWD control system.

Kallfass Sortierwerk Zuführung

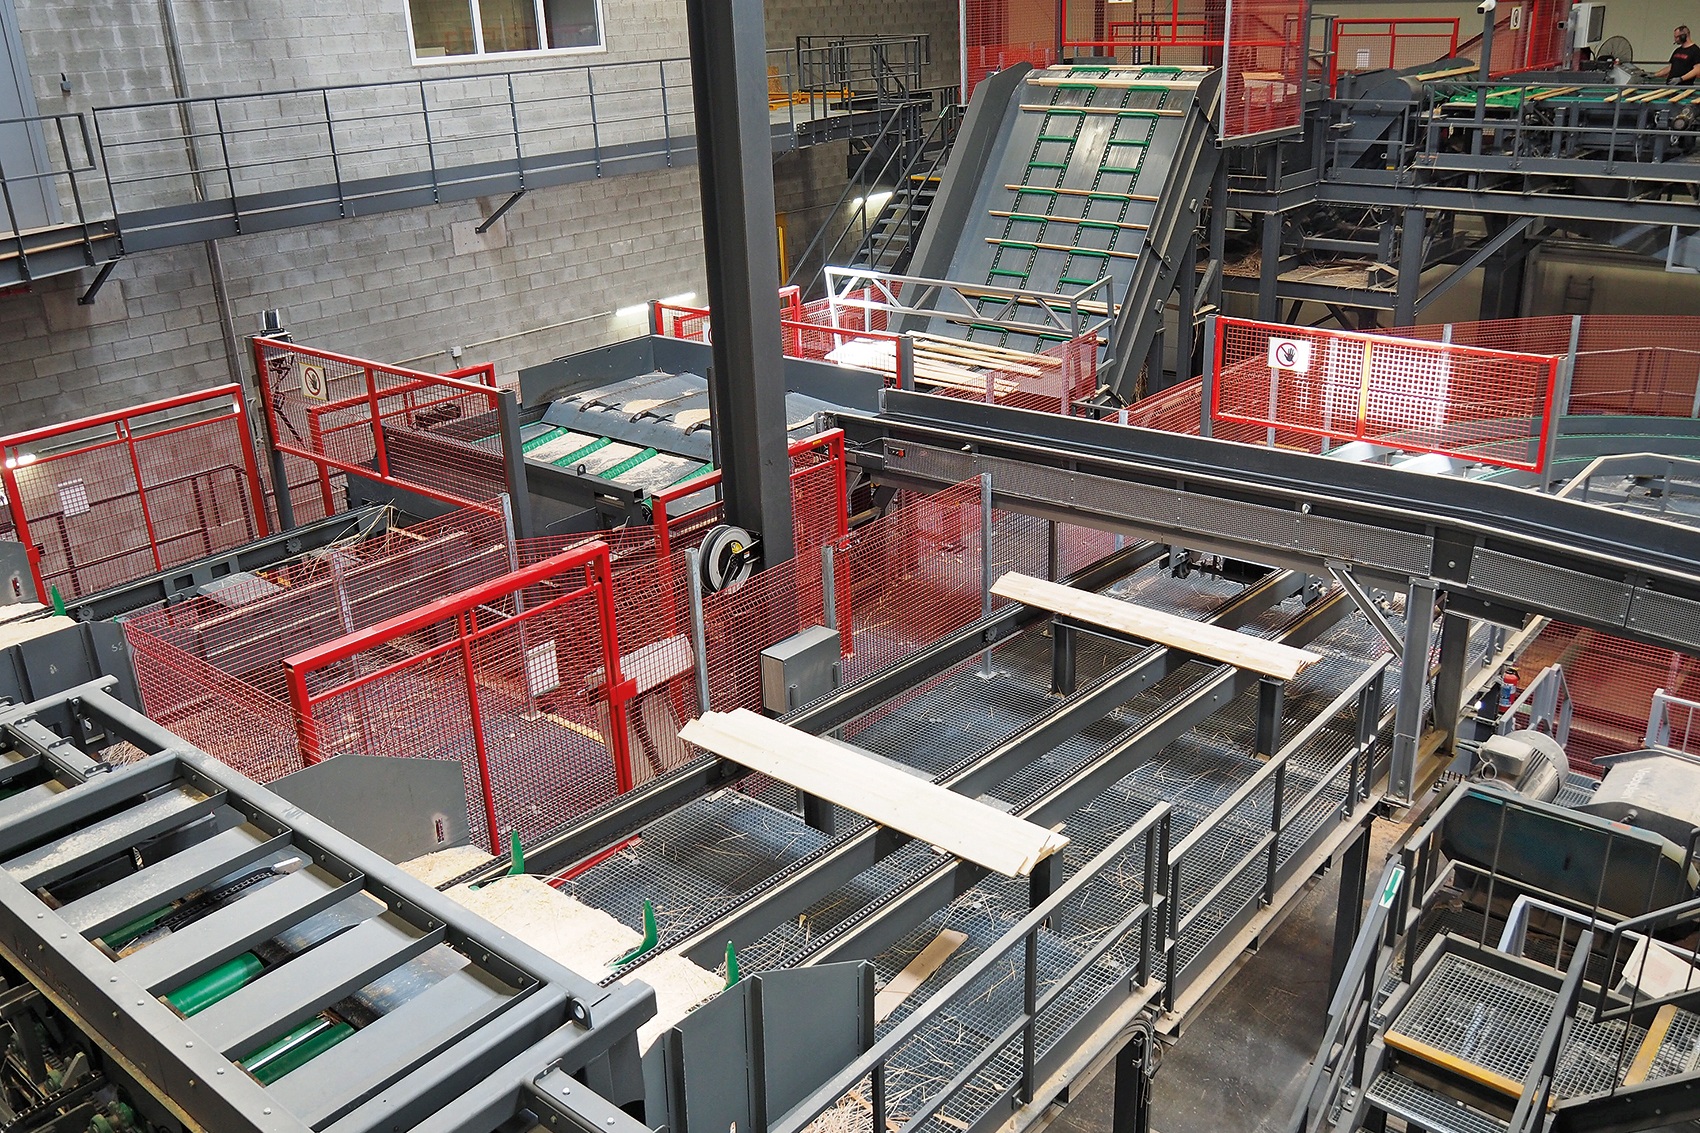
The sawn timber from the saw line is distributed across two Kallfass systems

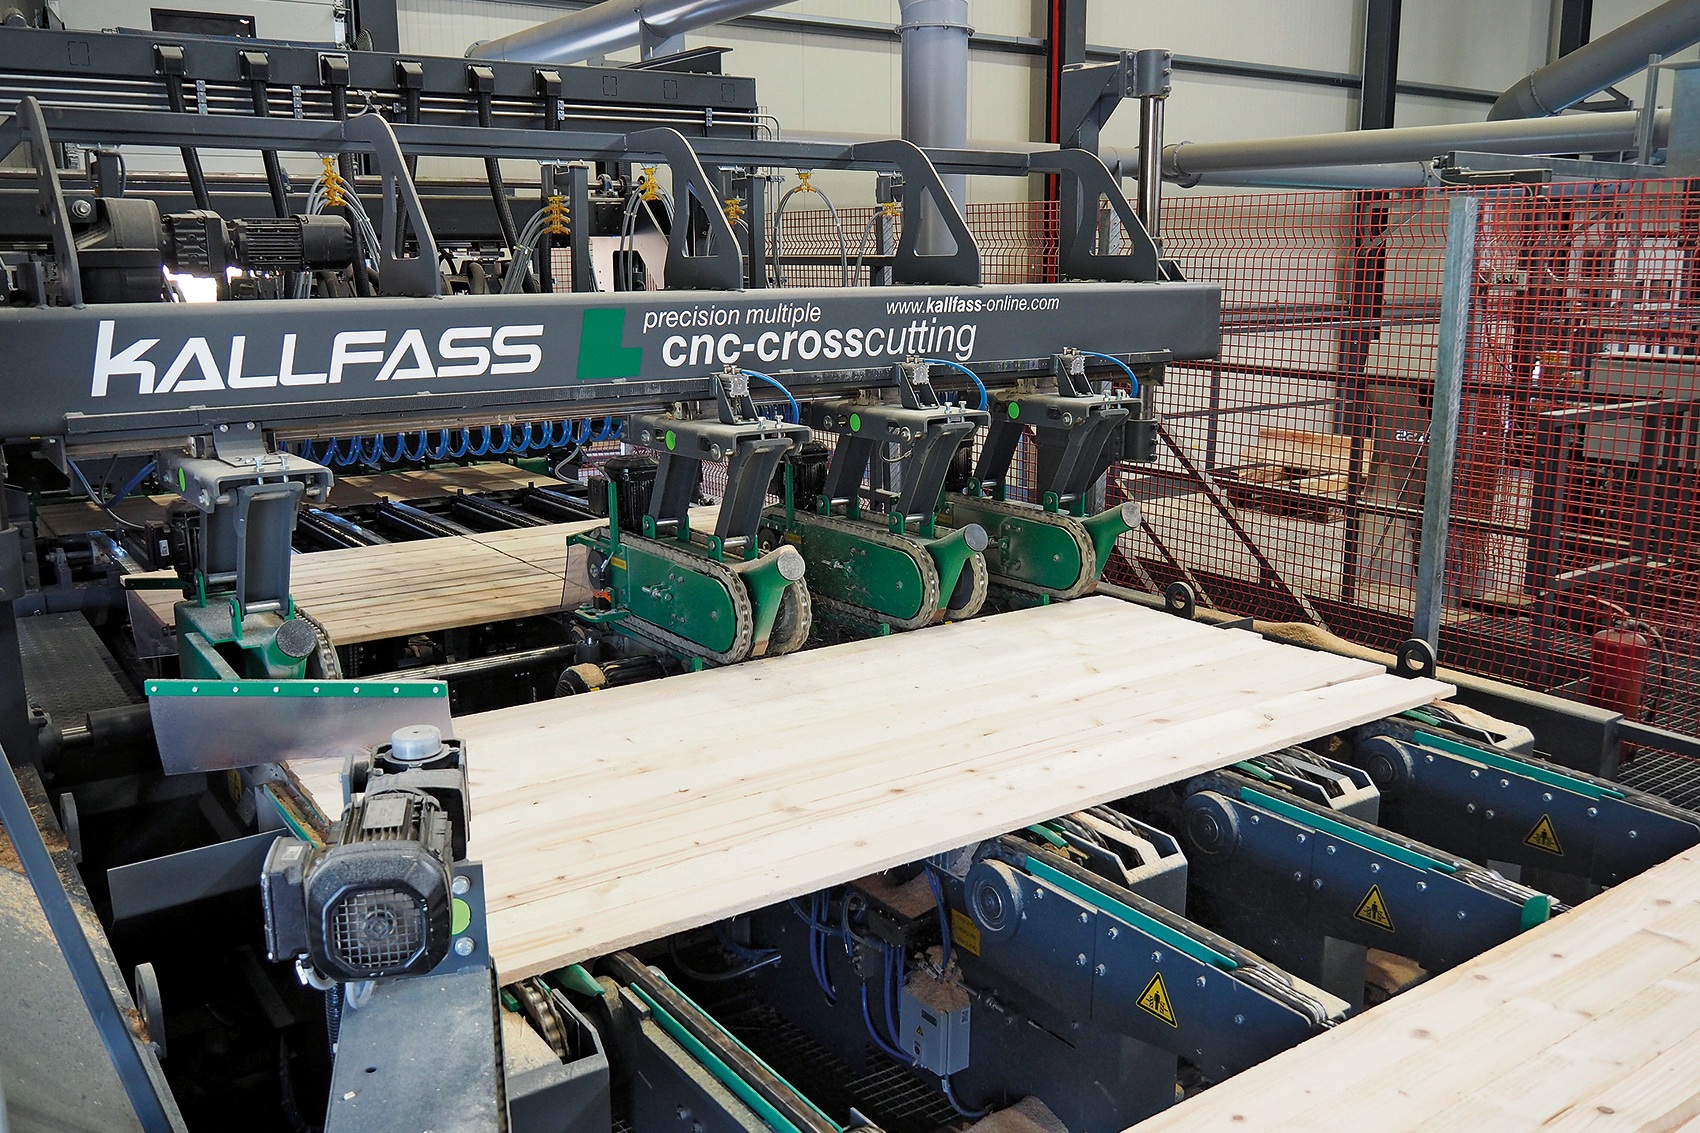
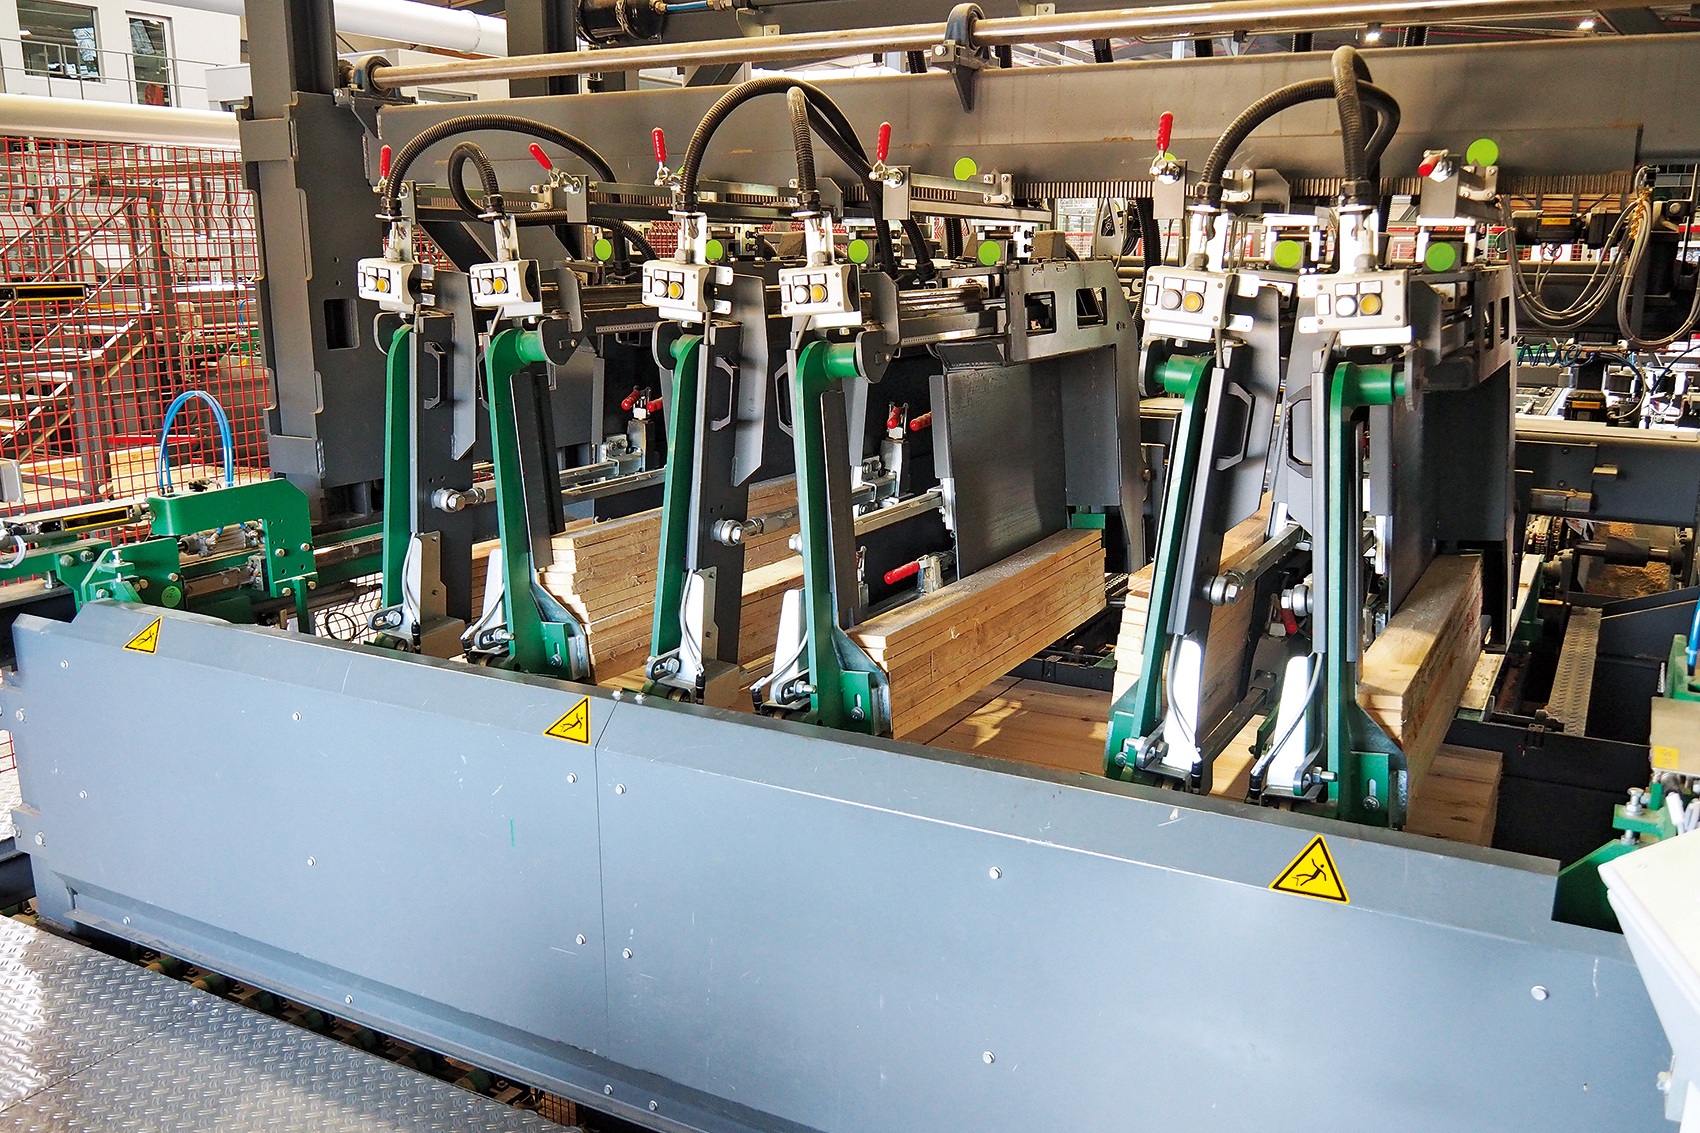
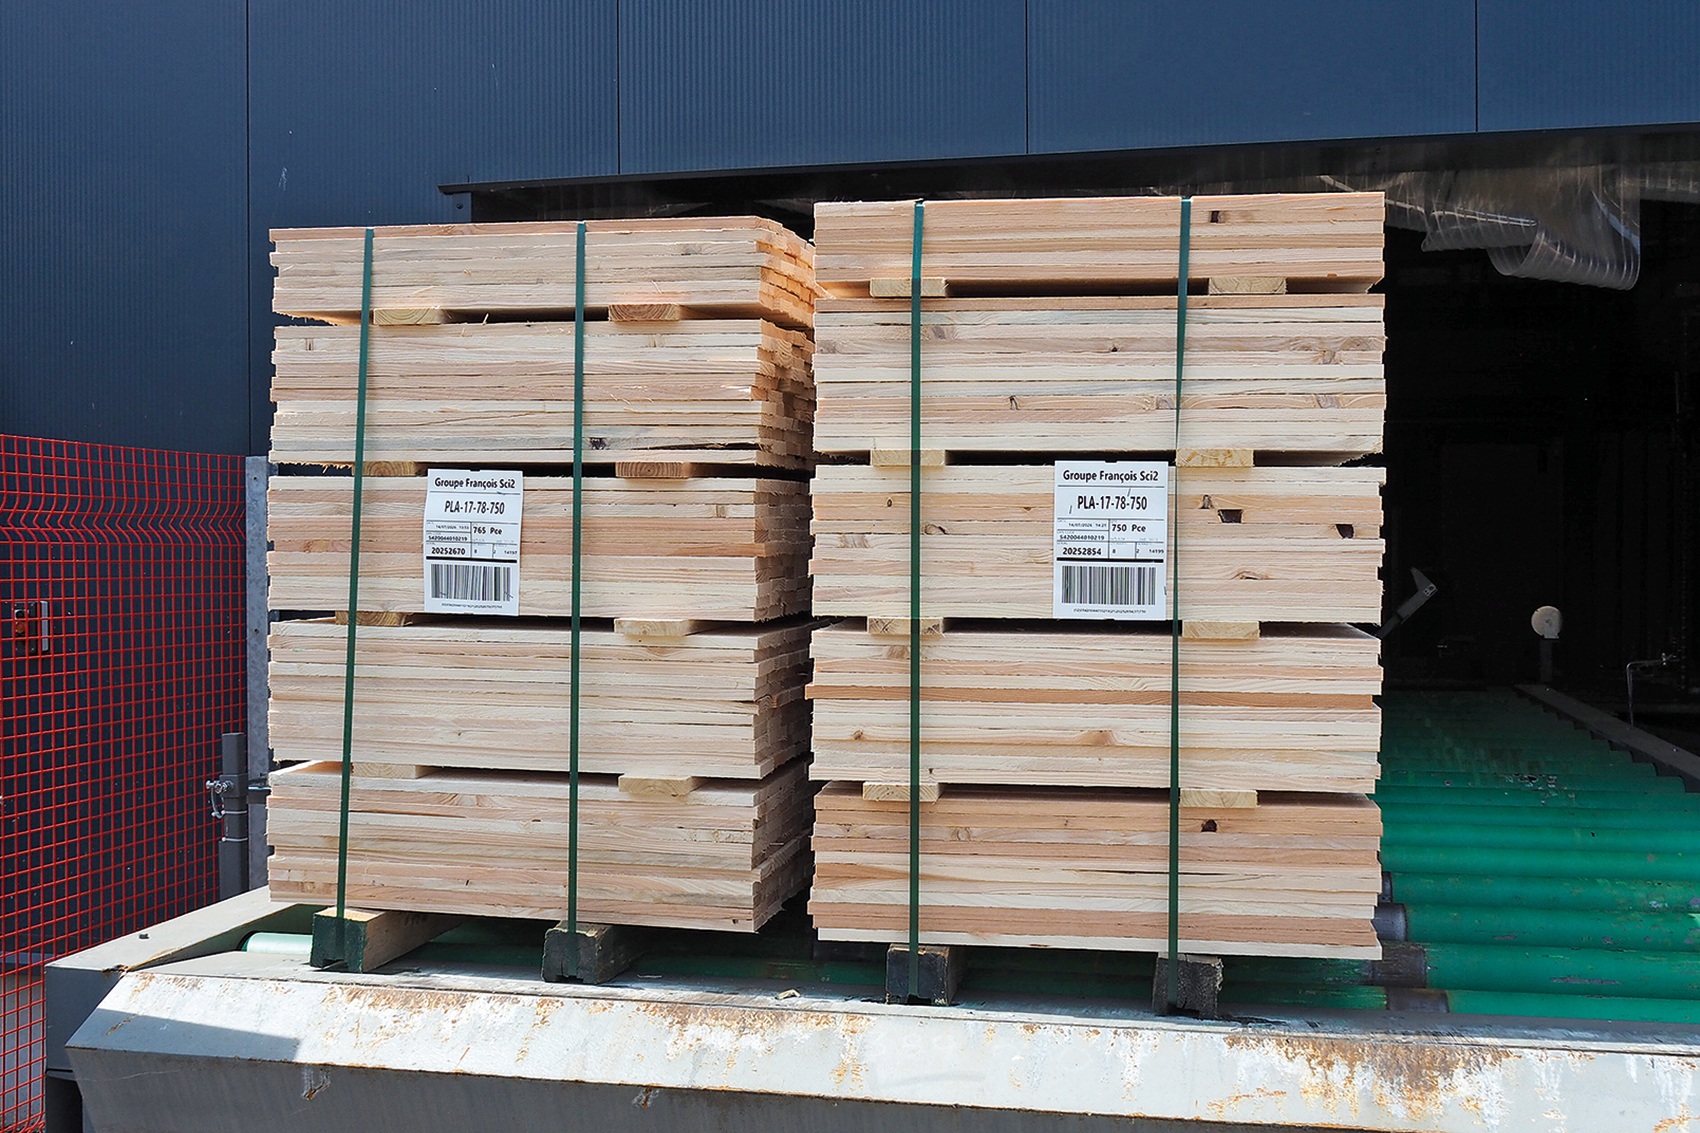
The standard material with a cross-section ranging from a minimum of 12 x 60 mm and a length of 2.1 to 2.5 m is drawn off to the left by the Kallfass handling system, transported across a long buffer section, and fed to the alignment roller conveyor. This is followed by layer creation. With the tried-and-tested multiple cross-cut saw from Kallfass, the goods can be cut to the desired length. The system is equipped with a fixed saw and three flexibly adjustable units. The downstream stacker with a capacity of up to 14 layers per minute has six magazines, which are manually filled with boards by the employees. The finished stacks descend via a hoisting unit onto a roller conveyor and are then strapped before being made available for transport.

Kallfass Mehrfachablängsäge

Proven multiple cross-cut saw from Kallfass with four saw aggregates – three units are variably adjustable

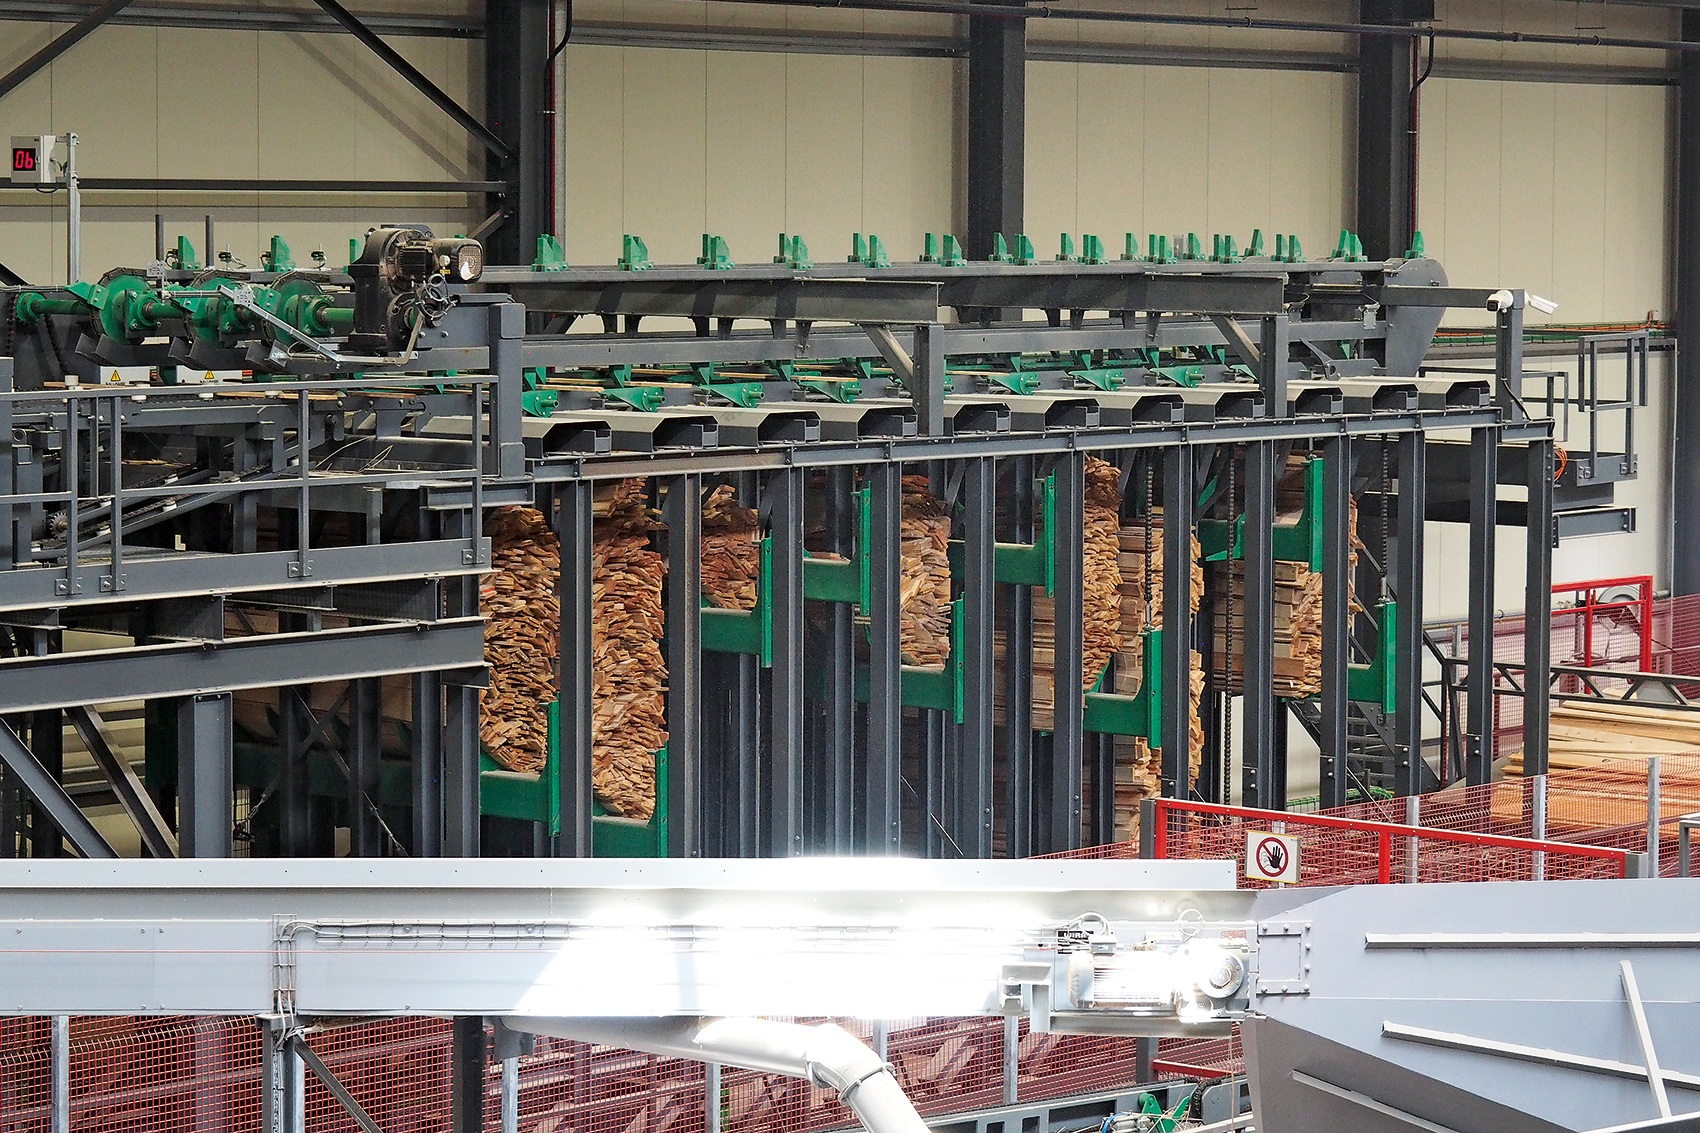
The sawn timber from the edger and resaw circular saw goes to the second Kallfass line. There, the boards are first separated. The operator assesses the quality and can, if necessary, reject individual pieces towards the disposal system. The following tong loader feeds the boards into the carrier conveyor. They are then measured in transverse flow. A scanner determines the wane. Based on these data, they are sorted into one of the ten boxes.

Kallfass Senkrechtboxen-Sortierwerk

Kallfass supplied a ten-box sorting system for line 2 at Groupe François

Once a box has reached the necessary fill level, it is emptied downwards. The conveyor brings the boards to a step separator and an unscrambler. Here, too, an employee checks the goods before the layers are created. Identical to the main line, Kallfass also installed a multiple cross-cut saw with four sawing units in this system. "All saw aggregates can also be swivelled down. The minimum cutting length is 600 mm", points out the Kallfass project manager points during the site tour. After passing through the stacking system – which is of identical design – the finished stacks reach a second strapping station and finally proceed to the discharge roller conveyor. The stacks can also be routed flexibly to either strapping unit in the event of a system failure. Both Kallfass systems are operated by just three employees, as Quoirin emphasises.

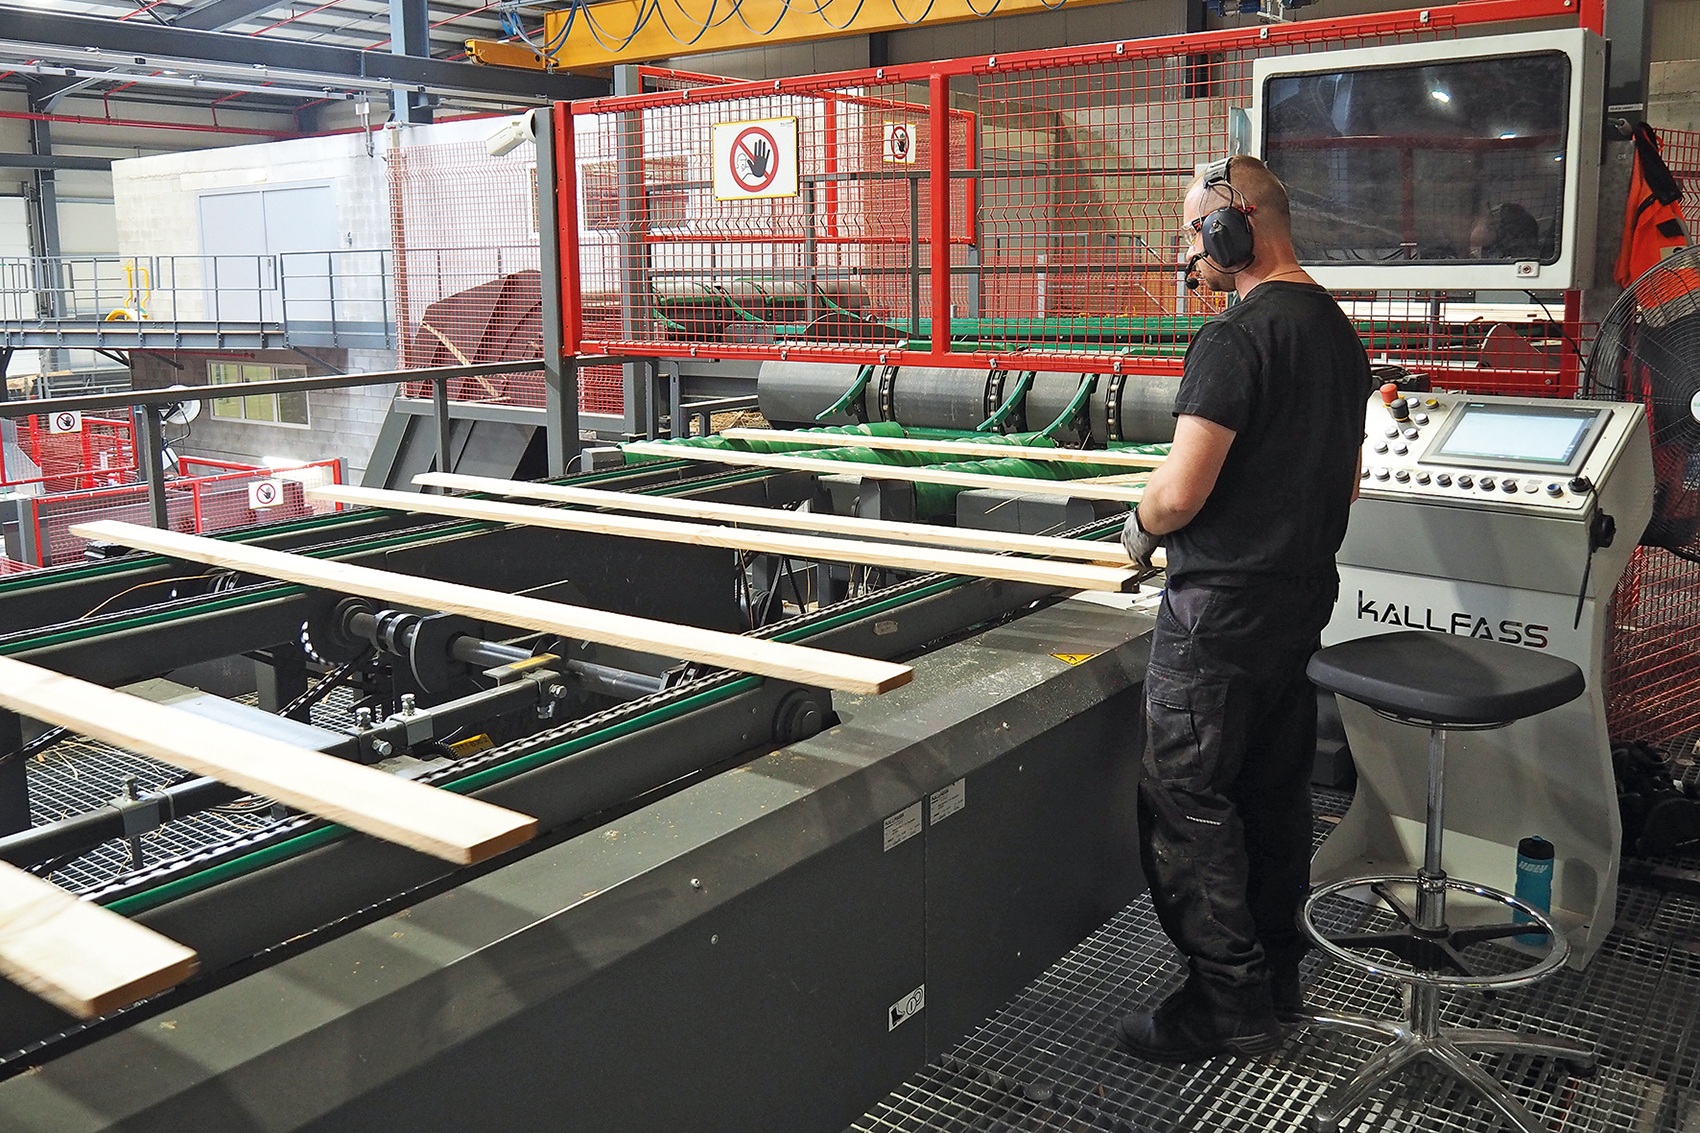
Kallfass Qualitätsbeurteilung

An employee assesses the timber, after which it moves on to sorting

Kallfass Sortier- und Stapelwerk

View of the systems running in parallel: In the foreground, the step separator following box sorting; on the right, the main line

Kallfass Brettmagazine

The stacking systems are equipped with automatic double magazines for boards

Kallfass stacked timber packs

The finished sawn timber packages are placed on the roller conveyor ready for removal.

Text and pictures: Martina Nöstler, Holzkurier

Holzkurier 34/2026

Zuschnitt- und Stapelanlage auf engem Raum EN Cutting and stacking system in a small space

Just over a year ago, the mechanisation specialist Kallfass from Baiersbronn-Klosterreichenbach in Germany installed a new cutting and stacking system at Woodfab Timber in Aughrim, Ireland. The challenge was to accommodate the system in an existing hall – including an external infeed for re-sorting.

In recent years, Woodfab Timber, founded in 1974, has continuously invested in increasing output and efficiency. One of the most recent projects was the expansion of the sorting line with a cutting and stacking system from Kallfass. "Sorting and stacking was a major bottleneck in our production. That's why we decided to invest in this area," explains Sean Brady, owner and managing director of Woodfab.

The sawmill is located in Aughrim on the east coast of Ireland, about an hour and a half by car south of Dublin. The company manufactures various products for fences, decking boards, posts and the packaging industry from softwood logs – almost exclusively spruce.

No bottleneck, more output

With the new Kallfass line, a bottleneck has now been eliminated. Stacking and cutting can be carried out by just one employee. Brady puts the output last year at around 110,000 m³, which represents a 10% increase compared to 2024. The plan for this year is 115,000 m³ in one shift. "This increased volume is only possible thanks to the new Kallfass system," Woodfab operations manager Richard White points out and he confirms: "We were able to significantly optimize our production process. Furthermore, we are now very flexible in production and our employees on the sorting line are no longer under so much pressure.”

Mr. Brady explained the decision to collaborate with the Baden-Württemberg-based specialist for the first time: "Kallfass listened, offered us the best solution and was able to perfectly implement our vision." Installation began in November 2024, and the line has been operational since February 2025. "Despite the challenge of integrating the new system into the existing production facilities, we didn't have a single day of downtime," Brady emphasized.

Sean Brady and Richard White

Satisfied with the project delivered by Kallfass: Woodfab Timber Managing Director Sean Brady (left) and Operations Manager Richard White (Pic. Woodfab)

Large variety of dimensions

Another key advantage of the new system is its wide range of cross-sectional and length capabilities: "It is designed for wood thicknesses from 16 to 150 mm and widths from 70 to 250 mm. Infeed lengths range from 2.1 to 3.8 m. At the stacking station, we can stack packages with lengths from 800 mm to 3.6 m," explains Kallfass project manager Matthias Link. Kallfass implemented the integration of the new stacking and cutting system into the existing sorting system with 35 boxes. The wood batches are fed onto a buffer chain conveyor with a swivelling device. "When swivelled down, the wood arrives at the stacking system. When swivelled up, the wood arrives on our new buffer conveyor, which is mounted under the existing system. The boards and squared timbers are then transferred to the curved conveyor," says Helge Widmann, responsible for design engineering at Kallfass.

The wood arrives at the aligning roller conveyor via an unscrambler with raised carriers for large cross-sections – designed without a step feeder for space-related reasons. After subsequent layer creation, the wood is fed to the Kallfass multiple circular cross-cut saw. The saw is equipped with five automatically positionable saw aggregates. The shortest cutting length is 800 mm. The offcuts fall onto a belt conveyor and are disposed of.

Kallfass has equipped the stacker with eight magazines for automatic stick placing. According to Matthias Link, the output is up to twelve board layers per minute. The special feature of the system is that it can also perform offset stacking for internal handling. Roller conveyors transport the wood packages to the strapping station, after which they are prepared for transport. The stacks are labelled for wood package tracking. "These labels show the quantity and dimensions, while the quality is entered manually by the employee," explains Matthias Link.
In addition, Kallfass supplied an external alimentation system with tilt destacking unit. After destacking, the lengths of wood are fed via a roller conveyor to the aforementioned unscrambler and stacked. The new system can also be used for re-stacking or re-sorting.

Kallfass unscrambling system

The sawn timber – coming from the boxes – is first separated. The carriers are raised for large cross-sections

"Expectations were exceeded"

The managers of Woodfab Timber and Kallfass both confirm that the collaboration between the two companies on the project was excellent. "With the new system, we can now respond to inquiries very quickly. Due to the wide range of dimensions it can produce, we are now very flexible and have additional capacity if needed. The high increase in output that is now possible with our Kallfass system has exceeded our expectations," confirms Mr. Brady.

Kallfass cross-cutting system

After layer creation, the timber is transported to the Kallfass multiple circular cross-cut saw

Kallfass stick placement system for wood packs

Kallfass supplied a stacker with automatic stick magazines

Kallfass destacking system

For re-sorting, Kallfass also installed an external alimentation system with tilt destacking unit at Woodfab Timber

Kallfass roller conveyor

These timbers are fed to the unscrambler via a roller conveyor

The packaging system can also perform offset stacking (Pic. Woodfab)

Text: Martina Nöstler, Holzkurier

Holzkurier 21/2026